

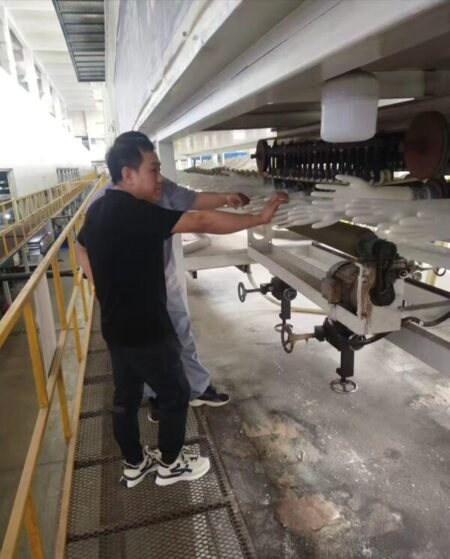
In the maintenance of a nitrile glove production line, the core objective of troubleshooting is to quickly identify abnormalities, precisely locate the fault, and minimize unplanned downtime through preventive maintenance. Troubleshooting capability directly affects the overall efficiency and product yield of the production line.
Electrical System Faults
When equipment frequently shuts down, சரிசெய்தல் should begin with three aspects: power supply, controller, and actuators.
1. Voltage instability can cause damage to circuit boards. A dedicated voltage stabilizer should be installed in the glove production workshop.
2. Check relays and contactors: Observe whether the relay contacts show signs of oxidation or blackening. Slight oxidation can be removed by polishing the contact surface with fine sandpaper to restore conductivity.
3. If the PLC fault indicator light remains on, first try restoring factory settings. If the fault persists, contact the manufacturer’s technical support.
Equipment Operation Troubleshooting
Material jamming in the மணிகள் வெட்டும் இயந்திரம்: When handling the fault, first stop the machine and clear the jammed material, then analyze the root cause, such as whether the lubrication status of the synchronizing gears meets the standard, or adjust the beading roller gap so that it is approximately 0.1 mm smaller than the glove thickness. If too tight, it will puncture the gloves; if too loose, the beading strength will be insufficient.
Uneven load torque distribution along long-distance chains can easily cause a “creeping” phenomenon. An idler wheel support can be installed on the slack side of the chain to tension the chain.
Production Process Troubleshooting
1. Pinholes on the glove surface
This is a common and most troublesome problem in nitrile glove production. Overall, it involves multiple factors: insufficient defoaming of the compound, excessively high vulcanization temperature, incomplete cleaning of the hand molds, etc. Each problem needs to be eliminated one by one to find the root cause.
2. Glove tearing and difficulty in demolding
This problem is usually determined by several factors: excessive demolding force or mechanism misalignment, over-vulcanization, burrs on the edge of the hand mold, etc., which need to be eliminated one by one.
3. Uneven thickness and dimensional deviation
This is usually related to தோய்த்தல் செயல்முறை parameters, such as whether the dipping time and withdrawal speed are stable, and regularly testing the coagulant concentration (e.g., calcium nitrate solution) to ensure uniformity. Wear of the hand mold dimensions can also cause dimensional deviation of the finished product, so the flatness of the hand molds needs to be calibrated regularly.
The above is a general troubleshooting plan during the operation of a nitrile glove production line. On-site troubleshooting may be more complex than these. For a continuous nitrile glove production line, the cost of reactive maintenance is far higher than that of preventive maintenance. If you have any questions about glove production lines, please contact our professional engineers at any time.
 Tamil
 English
 Arabic
 Hindi
 Thai
 Malay